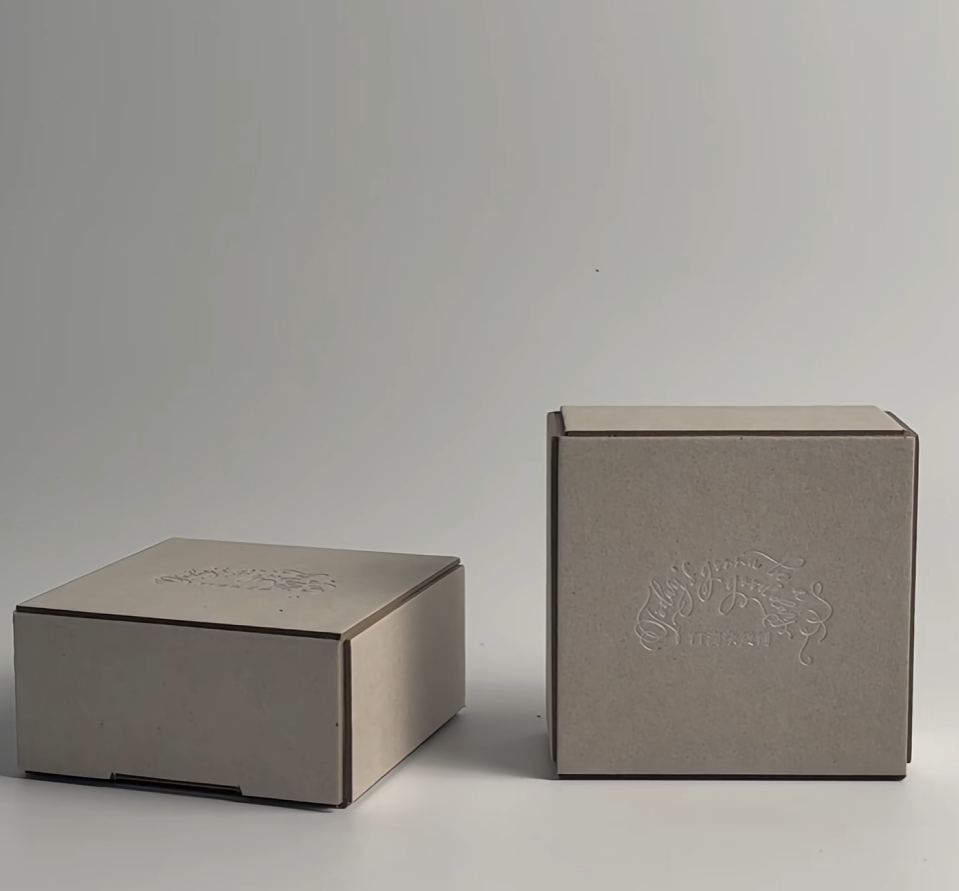
Selecting the right paperboard is one of the most critical decisions manufacturers and packaging professionals face today. The choice between different paperboard grades, thicknesses, and compositions directly influences production costs, product protection, environmental compliance, and overall brand perception. Getting paperboard selection right means balancing immediate budget constraints with long-term performance requirements, ensuring your packaging delivers both cost efficiency and reliability in real-world conditions.
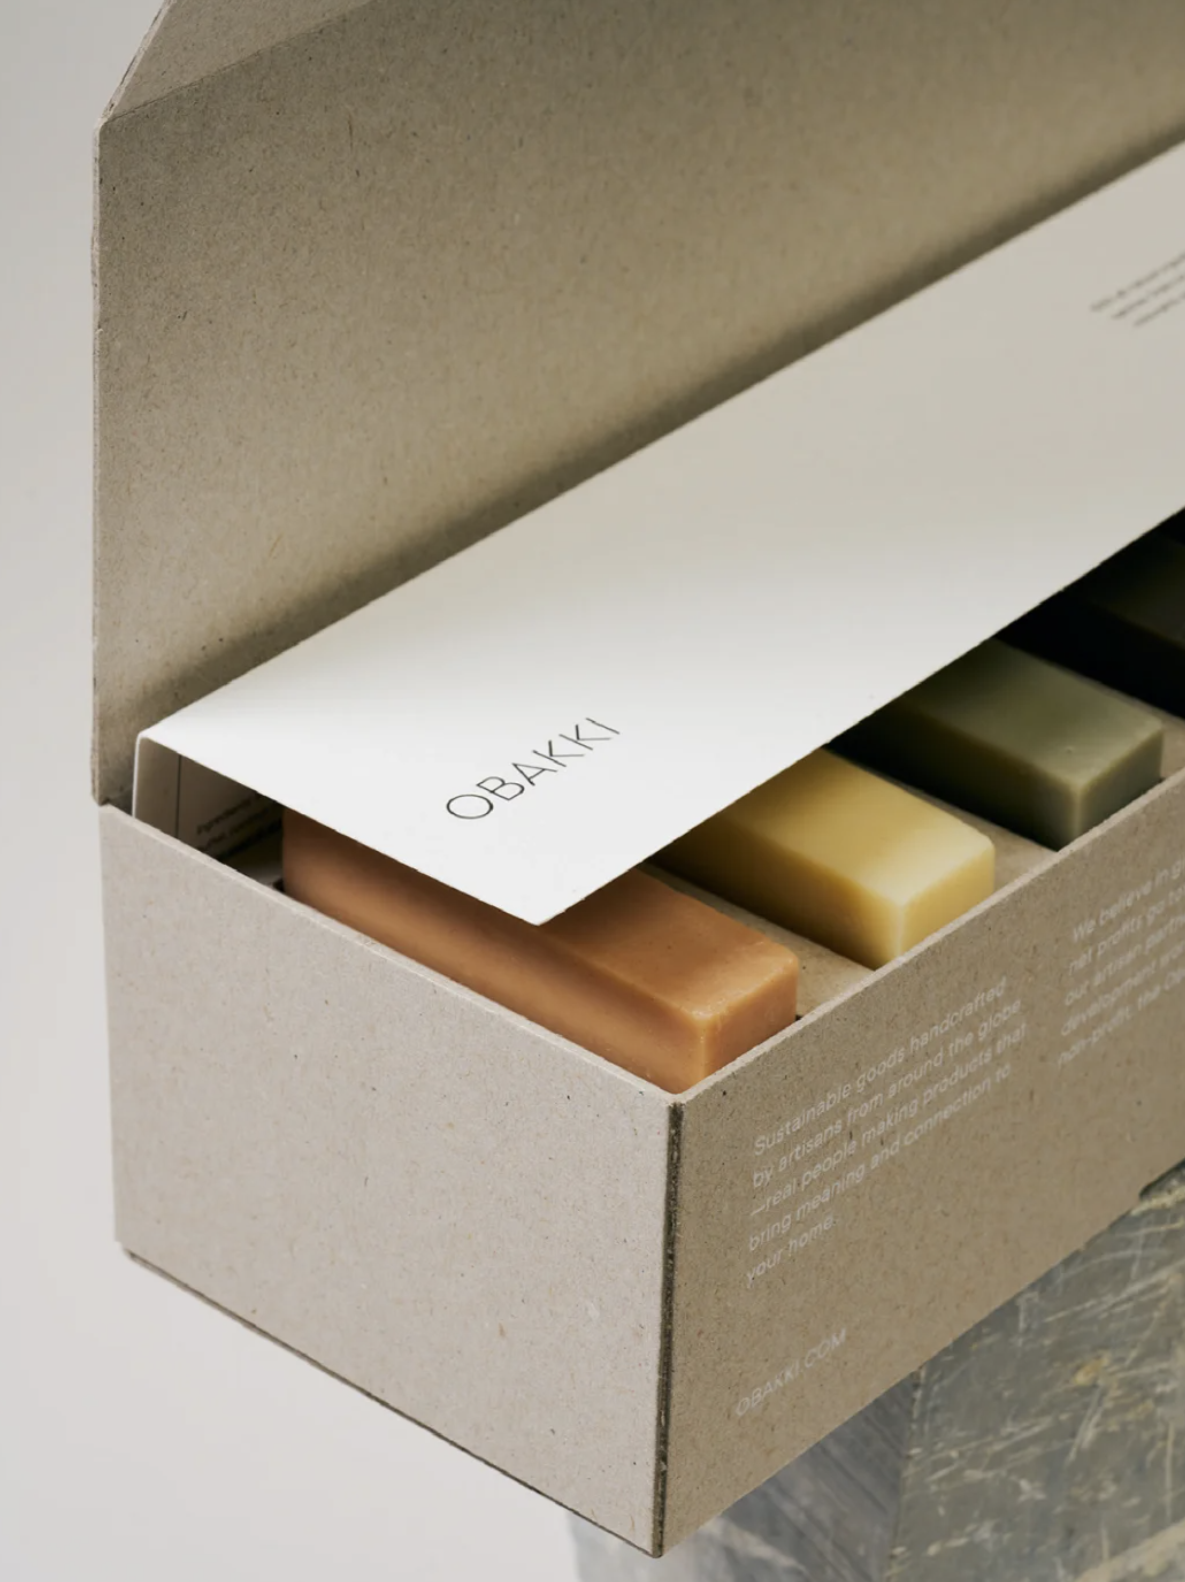
In today's competitive market, paperboard serves as far more than just a container. It protects contents during transit, preserves product integrity, communicates brand values, and influences customer purchasing decisions at the point of sale. Yet many organizations approach paperboard selection reactively, choosing the first available option or defaulting to previous specifications without evaluating whether they still meet current needs. This reactive approach often leads to either overspending on premium paperboard when standard grades would suffice, or cutting corners with inferior paperboard that fails under real-world conditions, resulting in product damage, customer complaints, and brand reputation risks.
The fundamental purpose of paperboard is protecting contents from physical damage, moisture, and environmental exposure. Different paperboard grades offer varying levels of structural integrity based on fiber composition, density, and coating systems. Folding carton paperboard, for instance, provides excellent stiffness and printability but may lack the moisture resistance needed for certain applications. Solid bleached board paperboard offers superior printability and aesthetic appeal, making it popular for premium packaging, while recycled fiber paperboard delivers adequate protection at lower cost for less demanding applications. Understanding these paperboard performance differences is essential because selecting paperboard with insufficient strength or moisture protection compromises the entire supply chain, from manufacturing through final customer receipt.
Modern paperboard must resist moisture, grease, oxygen, and light exposure depending on product requirements. Coated paperboard provides enhanced barrier properties through specialized surface treatments, while uncoated paperboard relies on fiber density alone. For food packaging, pharmaceutical products, or items exposed to humid environments, the right paperboard selection with appropriate barrier coatings prevents product degradation, extends shelf life, and maintains compliance with food safety regulations. Selecting paperboard without considering barrier requirements is a false economy that often results in product loss and customer returns that far exceed the initial material savings.
Strategic paperboard selection begins with precise application analysis rather than assumptions. A lightweight, cost-effective paperboard may be perfectly adequate for protective inner packaging or seasonal products, while premium paperboard might be justified for direct-to-consumer applications where brand perception drives purchasing decisions. This differentiated approach to paperboard selection allows organizations to optimize costs across their entire portfolio. For example, selecting premium recycled fiber paperboard for outer shipping boxes while using virgin fiber paperboard for visible consumer packaging represents intelligent cost management. Conversely, selecting high-performance specialty paperboard for internal components where standard paperboard would perform equally well represents wasteful overspending that impacts profitability without delivering measurable value.
Paperboard pricing is significantly influenced by order volumes, supplier relationships, and market conditions. Organizations that commit to consistent paperboard specifications enable suppliers to offer volume discounts, lock in favorable pricing, and maintain reliable supply. Frequent changes to paperboard grades, weights, or suppliers disrupt these relationships and increase procurement costs. However, the optimal approach involves periodically reviewing paperboard specifications to ensure they still align with current product requirements, manufacturing capabilities, and budget constraints. This balance between paperboard consistency and periodic strategic review prevents both supply chain inefficiency and premature cost increases from outdated specifications.
Consumer and regulatory pressure for sustainable packaging makes paperboard selection increasingly complex. Choosing recyclable paperboard, sustainably sourced virgin fiber, or certified recycled content paperboard aligns with environmental commitments and appeals to conscious consumers. However, these paperboard options often carry premium pricing that must be justified by brand positioning, customer willingness to pay, or regulatory mandates. The optimal paperboard selection strategy acknowledges that environmental performance, cost, and market positioning are interconnected. Organizations that transparently communicate their paperboard material choices and sourcing practices build brand trust, while those pursuing sustainability solely for marketing purposes risk reputation damage when authenticity is questioned.
Paperboard used for food contact must meet specific regulatory requirements including FDA approval, migration limits for chemical substances, and specific hygiene standards. Selecting non-compliant paperboard creates legal liability, supply chain disruptions, and potential product recalls that dwarf any material cost savings. Proper paperboard selection for food applications requires certification documentation, supplier verification, and often third-party testing. This regulatory dimension of paperboard selection is non-negotiable and must be evaluated before any cost considerations are made. Organizations that underestimate the importance of regulatory compliance in paperboard selection face consequences far more severe than the cost premium of approved materials.
Paperboard thickness directly influences protective capacity, production speed, and material cost. Thicker paperboard provides superior protection and creates a more premium feel but increases material consumption and shipping weight. Thinner paperboard reduces costs and environmental impact but may offer insufficient stiffness or protection. The optimal paperboard thickness depends on product weight, fragility, transportation distance, and shelf display requirements. Selecting paperboard thickness too thin risks product damage, while selecting it too thick wastes material and budget. Most applications benefit from rigorous testing to determine the minimum paperboard thickness that reliably protects contents under actual logistics conditions.
Paperboard coating quality directly affects printability, durability, barrier properties, and aesthetic appeal. High-quality coatings enable vibrant color reproduction, fine detail printing, and resistance to scuffing during handling. Paperboard with inferior coating quality shows smudging, color variation, and reduced moisture resistance, compromising both brand presentation and product protection. The coating represents a significant portion of overall paperboard cost, making it tempting to reduce coating specifications to lower prices. However, selecting paperboard with substandard coatings often backfires through returned products, customer complaints, and damaged brand reputation that far exceeds the initial material savings.
Organizations should periodically review paperboard specifications when product changes occur, supply chain disruptions create sourcing challenges, customer feedback indicates protection inadequacies, or cost reduction initiatives are implemented. Market changes in paperboard pricing may justify switching to different suppliers or grades. However, frequent, unplanned changes to paperboard specifications create manufacturing disruptions, quality inconsistencies, and supply chain inefficiencies. Strategic paperboard reviews should occur during scheduled procurement cycles, ideally quarterly or semi-annually, allowing sufficient time to test alternatives, negotiate new supplier agreements, and implement changes without disrupting production. Planned, deliberate changes to paperboard specifications deliver better outcomes than reactive emergency switches driven by supply problems or budget crises.
 EN
 Request An Estimate
 Projects
