Holographic Paper - Security & Visual Solutions

One free digital sample for orders over $500
For orders over $7,500, a voucher worth $500 will be given, which can be deducted from the next big shipment or proof.

holographic paper

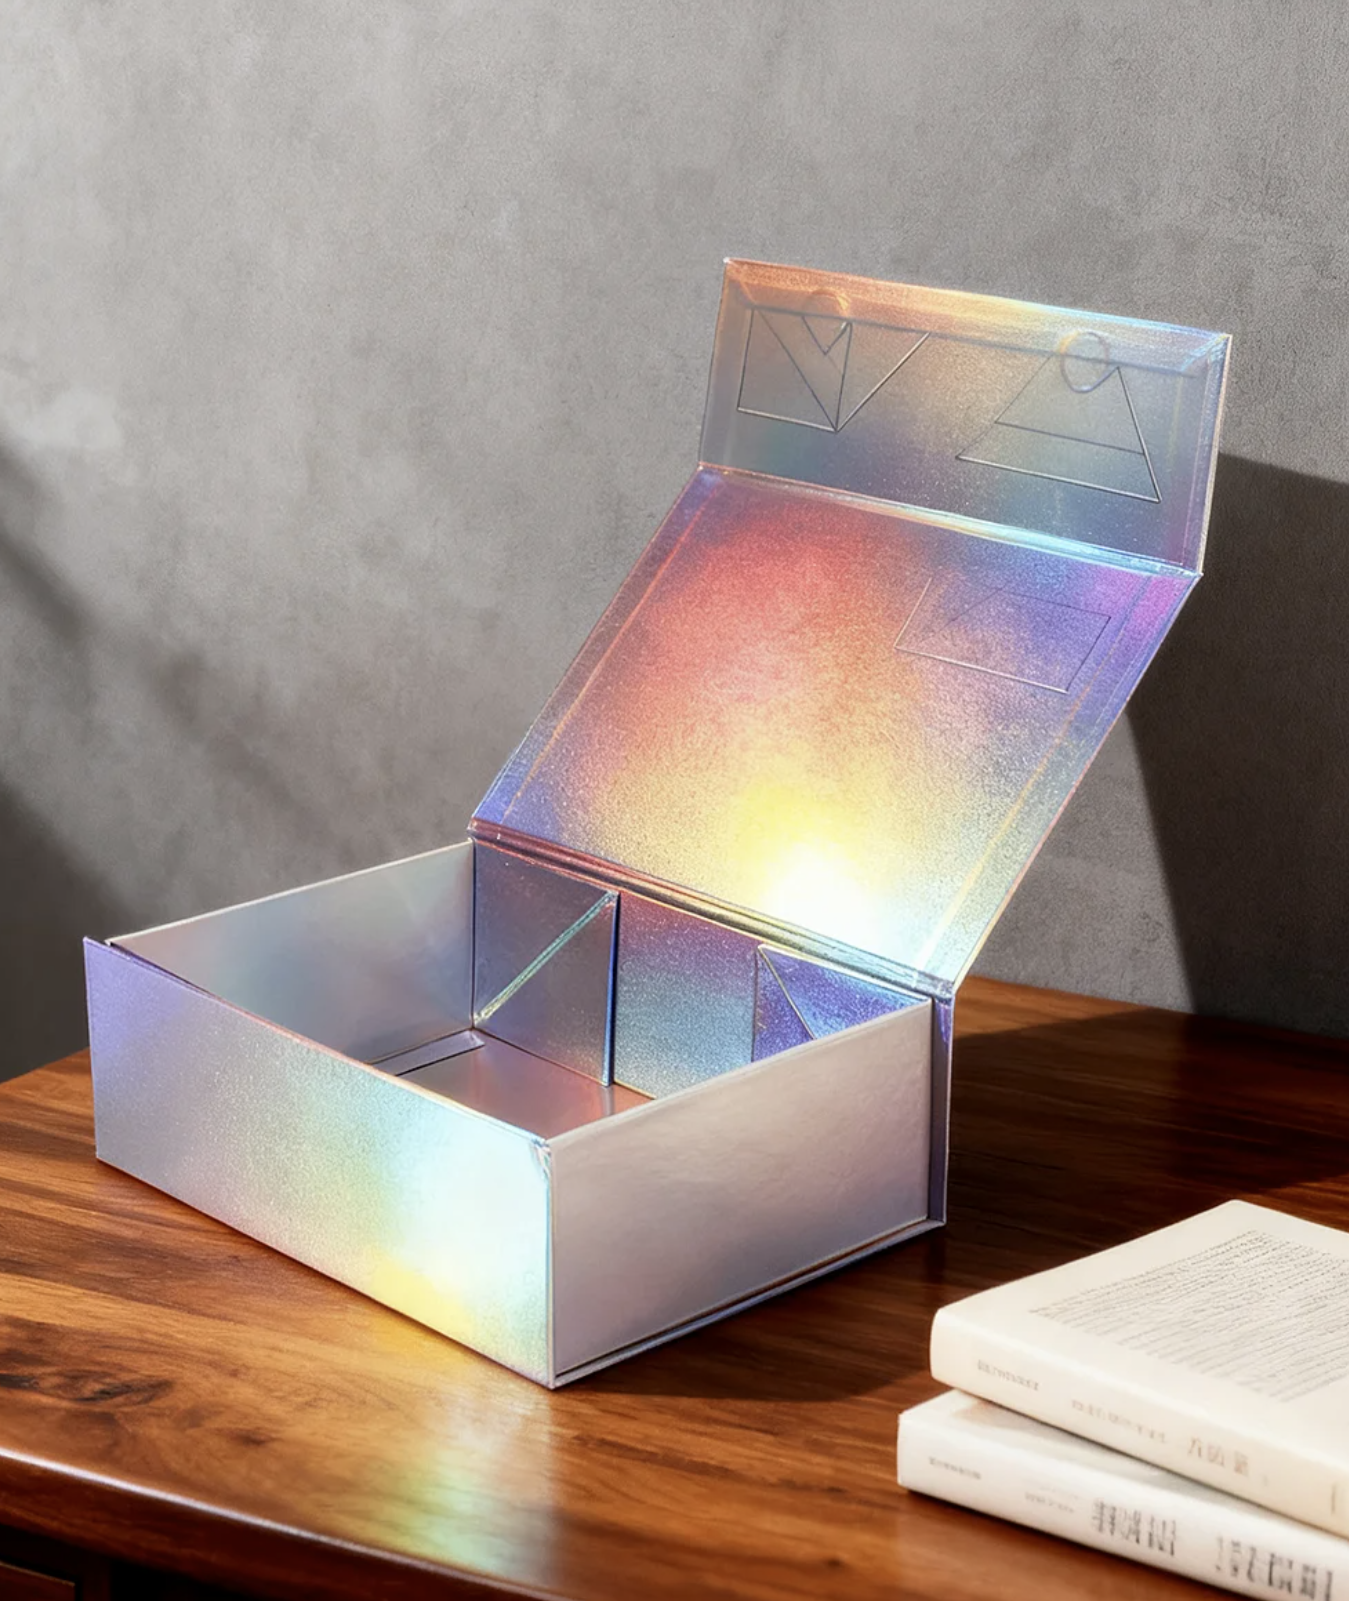
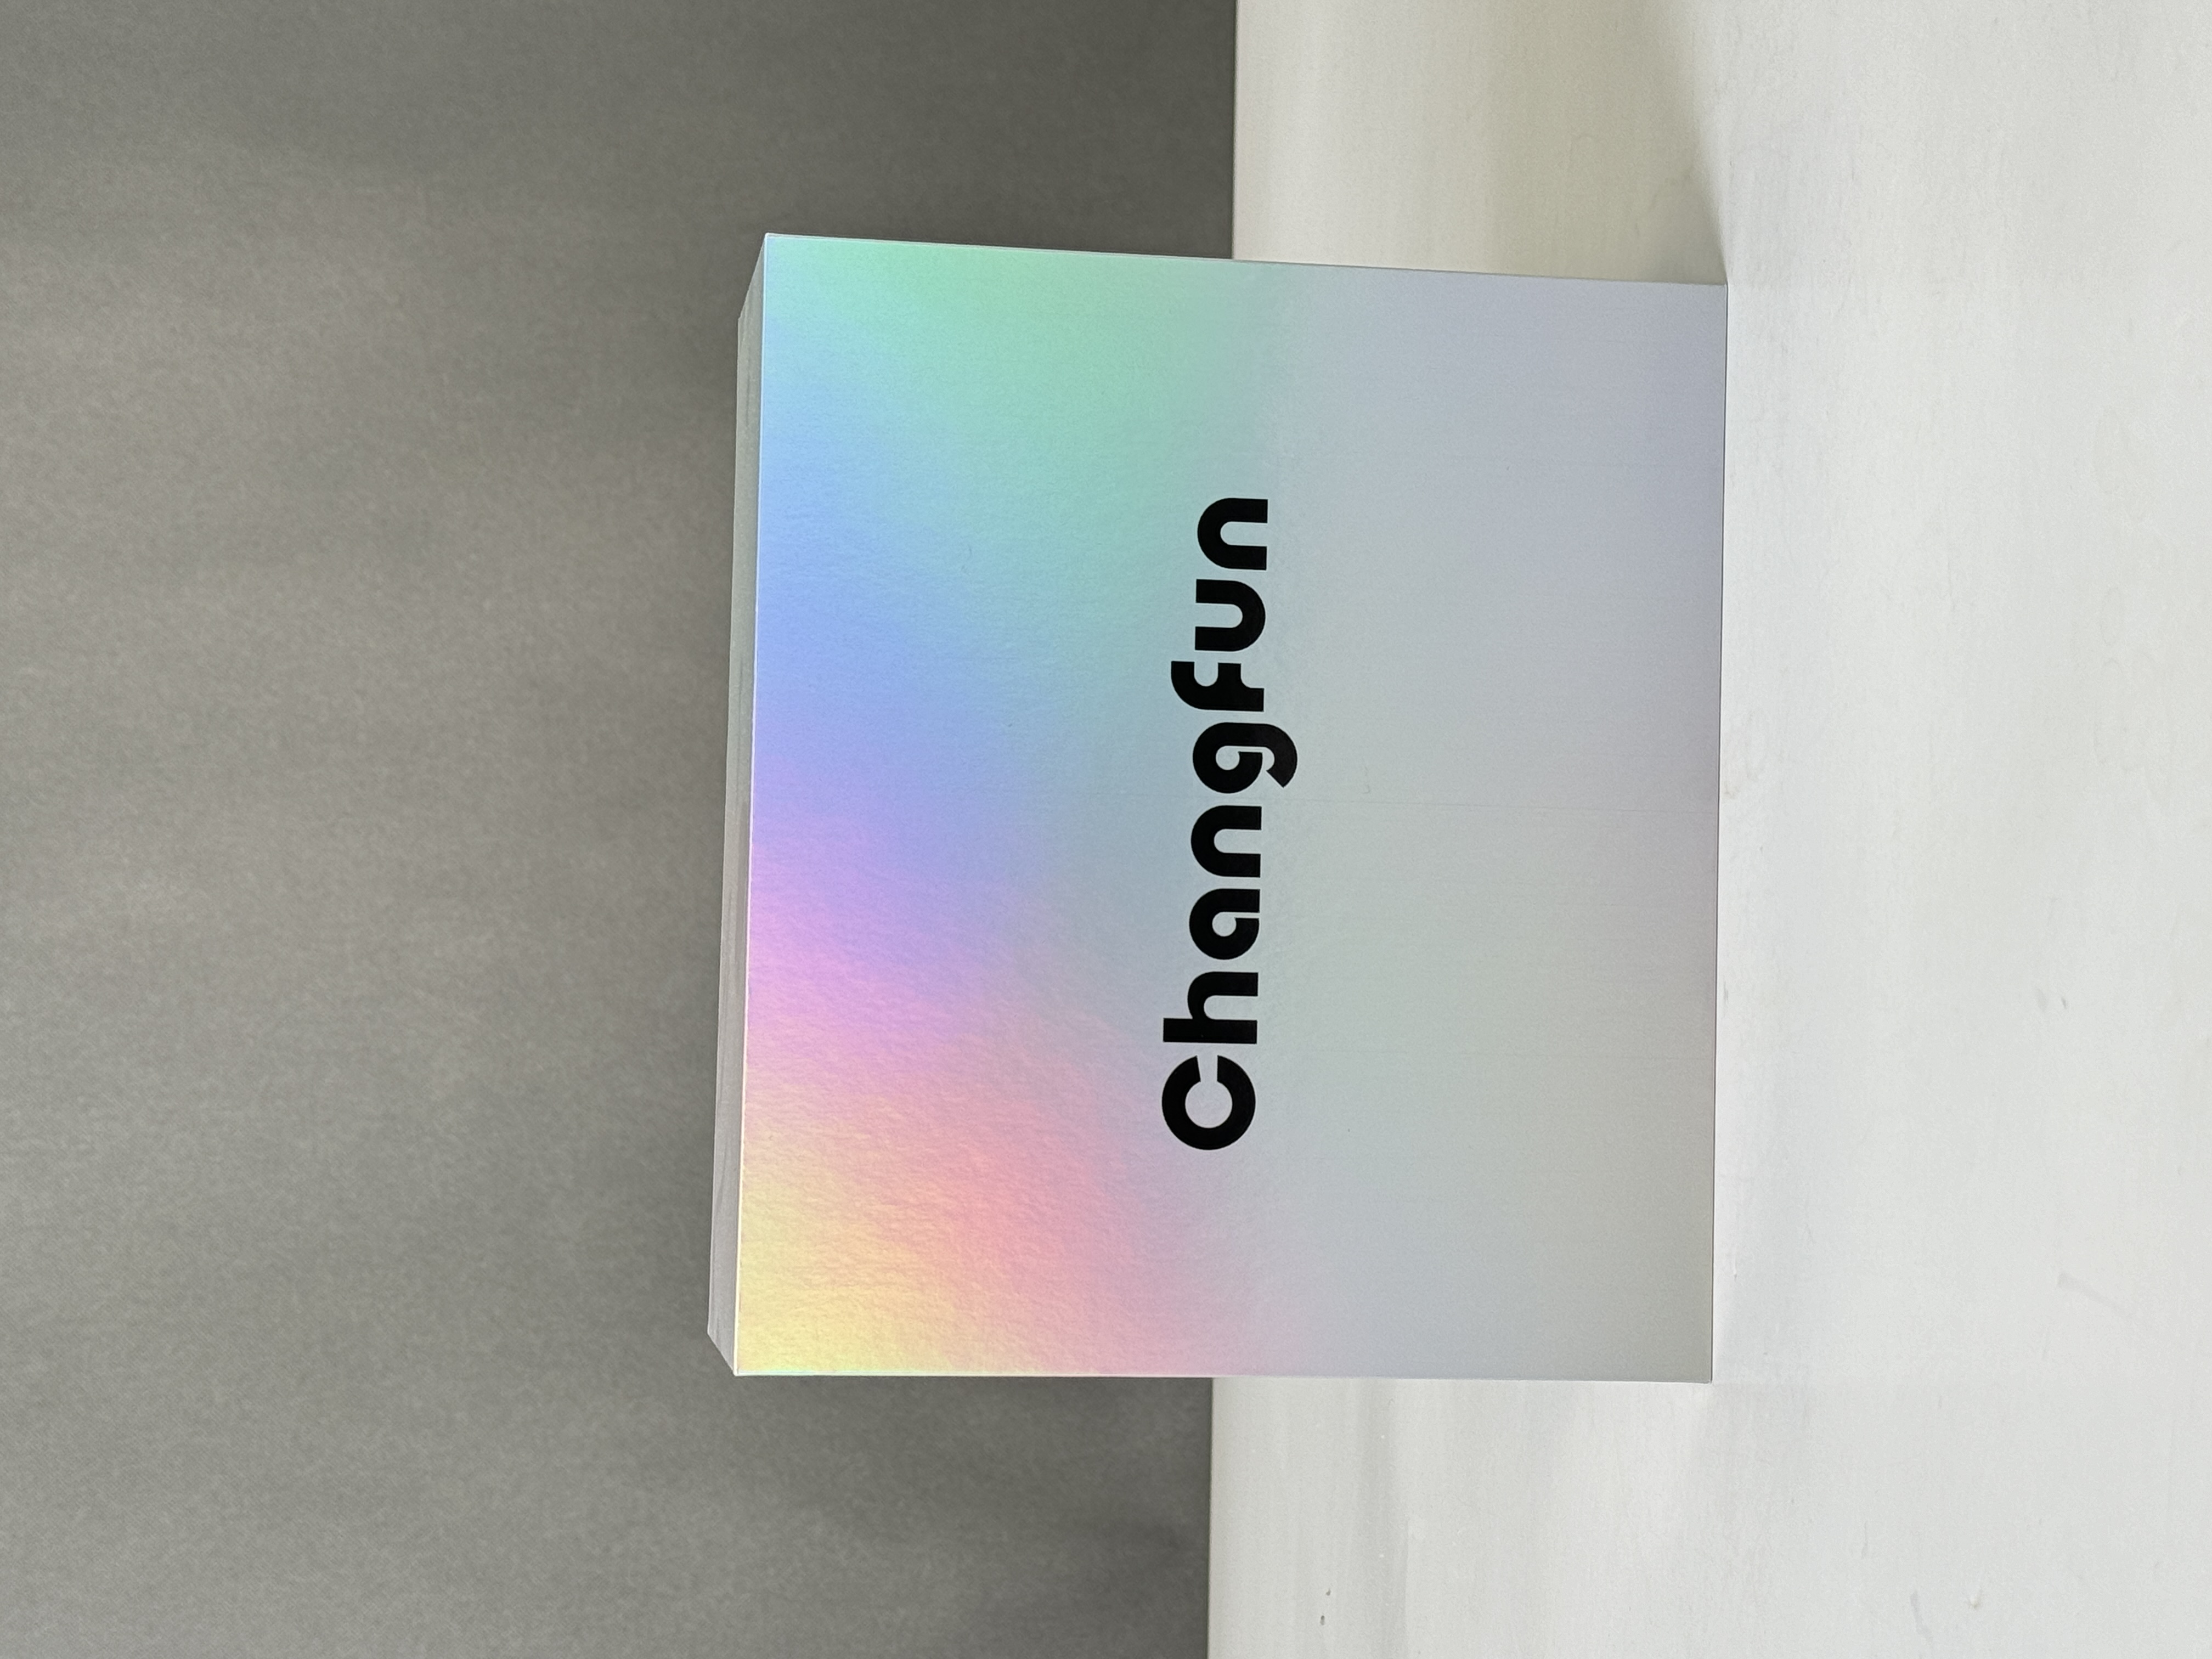
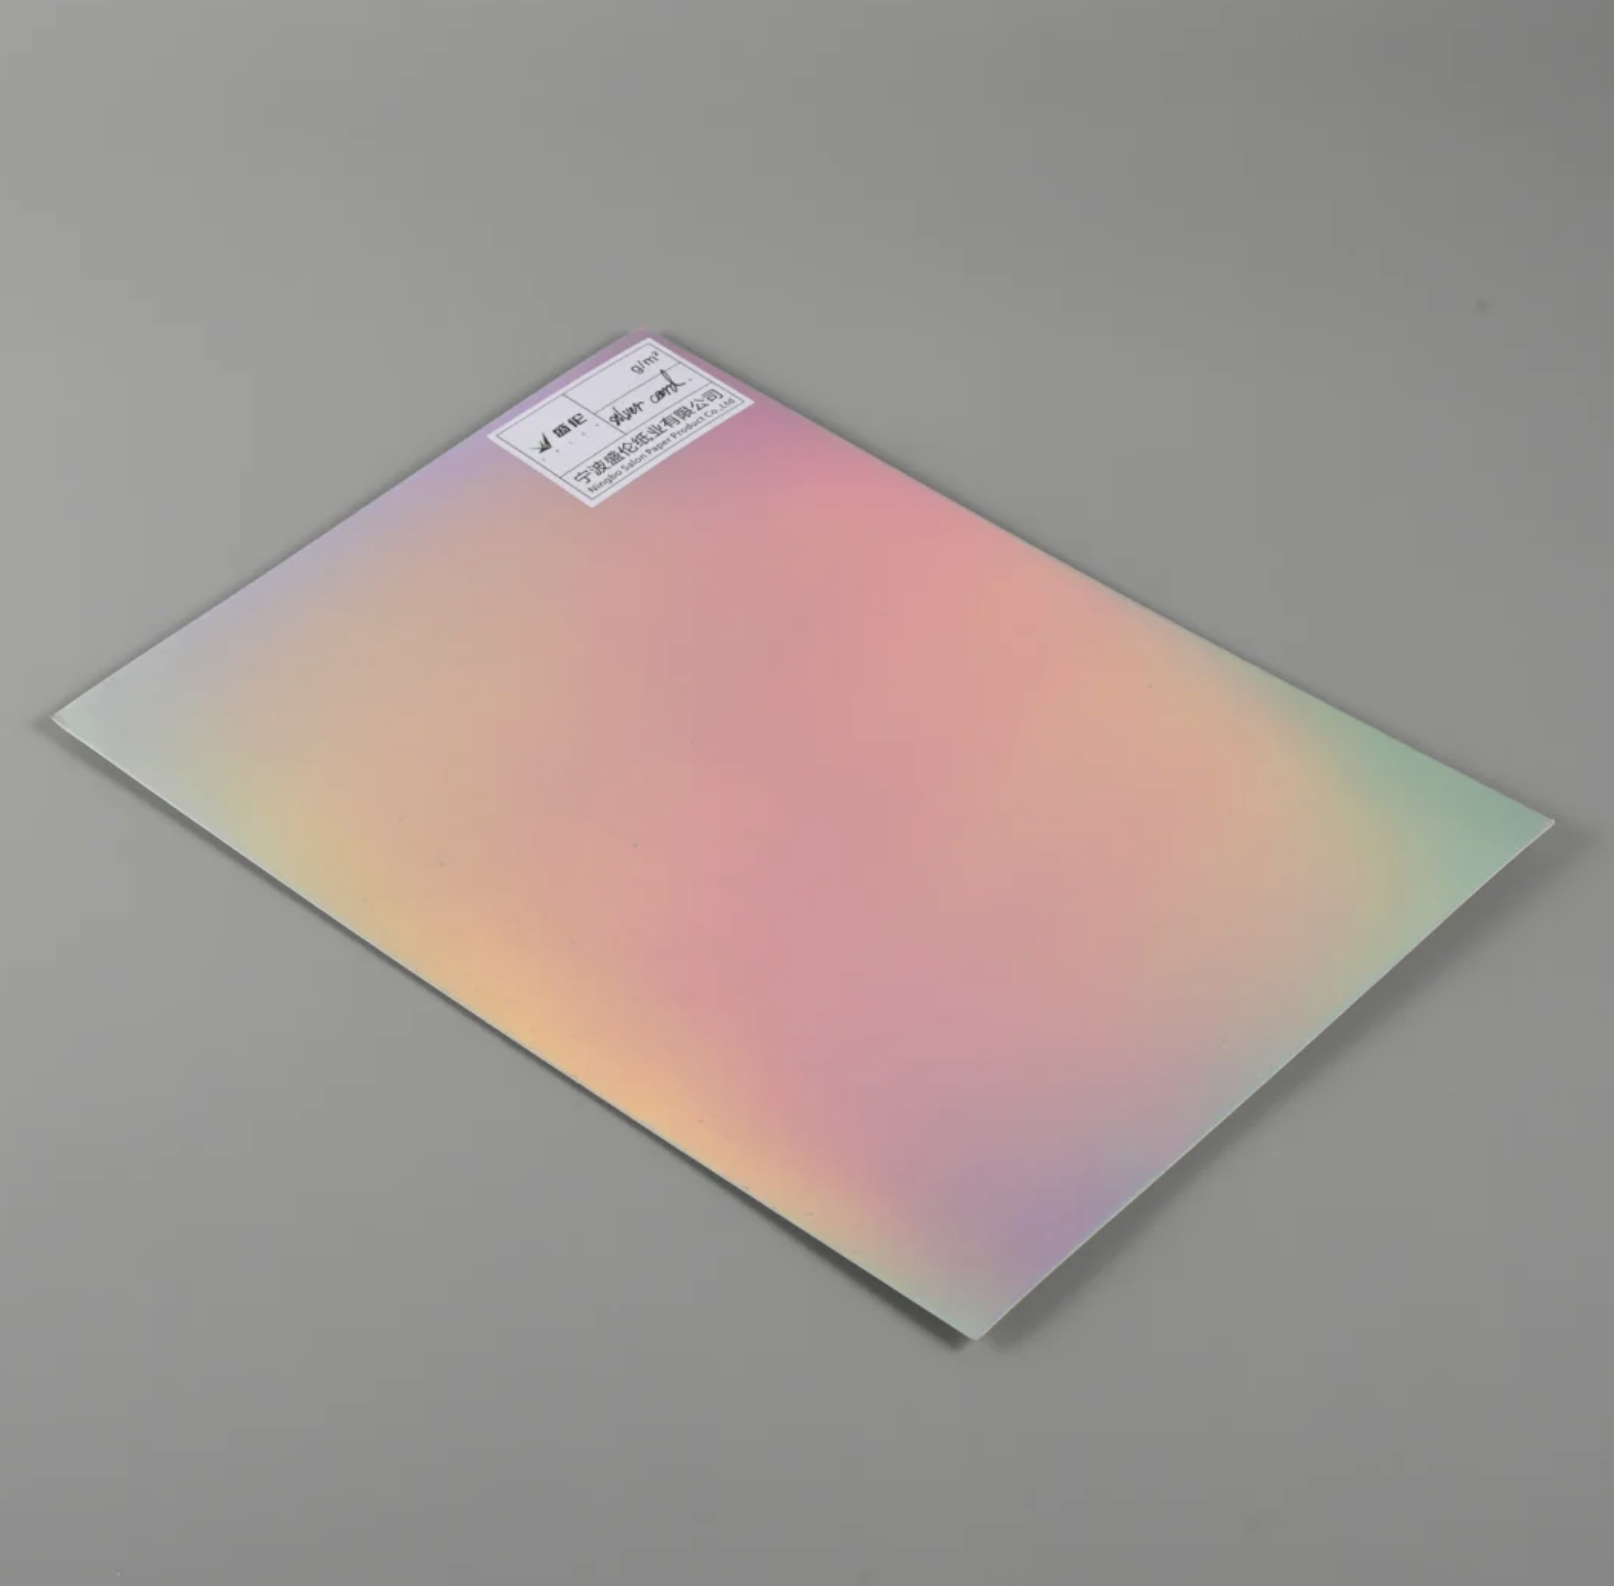
Holographic paper is an innovative specialty material that features a distinctive three-dimensional visual effect created through advanced light diffraction technology. This premium substrate incorporates microscopic patterns embossed or laminated onto its surface, producing stunning rainbow-like reflections and dynamic color shifts when viewed from different angles. Holographic paper serves multiple essential functions including brand protection, aesthetic enhancement, and product differentiation in competitive markets. The technological foundation relies on precision interference patterns that manipulate light wavelengths, creating eye-catching optical illusions without requiring special viewing equipment. Manufacturers produce holographic paper through various methods including hot stamping, lamination, and direct coating processes, each offering distinct visual characteristics and durability levels. This versatile material finds widespread applications across packaging design, security printing, promotional materials, gift wrapping, and decorative arts. The paper substrate can be customized with different holographic patterns ranging from geometric designs to custom brand-specific imagery, providing businesses with unique identification solutions. Modern holographic paper also integrates with digital and offset printing technologies, allowing for seamless incorporation into existing production workflows. Environmental considerations have driven recent innovations, with recyclable and biodegradable holographic paper options now available to meet sustainability requirements. The material's ability to combine functional security features with striking visual appeal makes holographic paper an invaluable resource for brands seeking to elevate product presentation while protecting against counterfeiting and unauthorized reproduction in today's demanding marketplace.
New Product Releases

Choosing holographic paper delivers immediate visual impact that captures consumer attention and distinguishes your products from competitors on crowded retail shelves. The material creates premium perception without requiring expensive printing techniques, as the holographic effect itself communicates quality and value to potential buyers. You gain built-in security features that deter counterfeiters and protect brand integrity, since replicating authentic holographic patterns requires specialized equipment and expertise that unauthorized producers typically cannot access. This protective characteristic proves especially valuable for luxury goods, pharmaceuticals, cosmetics, and electronics where brand authenticity directly influences purchasing decisions. Operationally, holographic paper integrates smoothly with standard printing and converting equipment, minimizing production disruptions and additional capital investment. The material accepts various printing methods including flexography, offset, and digital printing, allowing you to maintain existing workflows while upgrading product appearance. You benefit from exceptional versatility as holographic paper suits diverse applications from primary packaging to promotional inserts, labels, certificates, and event materials. The dynamic visual effects remain effective under different lighting conditions, ensuring consistent brand presentation across varied retail environments and consumer touchpoints. Cost efficiency emerges as another practical advantage since holographic paper provides multiple benefits within a single material choice, eliminating the need for separate security features or premium coatings. Environmental responsibility becomes achievable with recyclable holographic paper options that meet sustainability goals without sacrificing visual impact or protective capabilities. The material's durability ensures printed designs and holographic effects withstand normal handling, storage, and transportation conditions, maintaining product presentation quality throughout the supply chain. These combined advantages make holographic paper a strategic investment that enhances brand value, protects market position, and delivers measurable return through increased consumer engagement and purchase conversion.

Latest News

How to Cut Product Packaging Costs Without Compromise

15

Dec

How to Cut Product Packaging Costs Without Compromise

Modern businesses face mounting pressure to reduce operational expenses while maintaining quality standards, and product packaging represents one of the most significant opportunities for cost optimization. Smart companies are discovering innovative ...
View More
Product Packaging Design: A Complete Guide

15

Dec

Product Packaging Design: A Complete Guide

In today's competitive marketplace, product packaging serves as the silent salesperson that can make or break a brand's success. Beyond its fundamental role of protection and containment, effective product packaging design has evolved into a sophisti...
View More
Top 10 Designer Perfume in Box Collections

15

Dec

Top 10 Designer Perfume in Box Collections

Designer perfumes have always captivated fragrance enthusiasts with their exquisite scents and luxurious presentations. The art of packaging these precious liquid treasures has evolved into a sophisticated blend of protection, aesthetics, and brand s...
View More
How Do Printing Solutions Adapt to Different Material Applications?

30

Jun

How Do Printing Solutions Adapt to Different Material Applications?

Modern manufacturing and branding demands require printing solutions that can perform consistently across a wide variety of substrates and surfaces. From rigid cardboard to flexible film, from coated art paper to woven fabric, every material responds...
View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Interested Products
Please enter your interested products
Message
0/1000

holographic paper

Advanced Anti-Counterfeiting Protection

Advanced Anti-Counterfeiting Protection

Holographic paper provides sophisticated security features that effectively combat product counterfeiting and unauthorized reproduction attempts. The complex optical patterns embedded within the material require specialized holographic origination equipment and expert technical knowledge to create, establishing significant barriers against counterfeit operations. These intricate light-diffracting structures cannot be accurately reproduced using standard printing or photocopying equipment, making authentication straightforward for both enforcement authorities and end consumers. Businesses implementing holographic paper gain multiple layers of protection as the visible holographic effects serve as immediate authentication indicators while microscopic pattern details offer forensic-level verification capabilities. This dual-level security proves particularly critical for industries facing substantial counterfeiting threats including pharmaceuticals, luxury accessories, electronics components, and licensed merchandise. The overt nature of holographic security features also provides psychological deterrence, discouraging counterfeiters from targeting protected products due to increased detection risks. Implementation costs remain reasonable compared to other advanced security technologies, making holographic paper accessible for businesses across various scales. The material maintains its protective effectiveness throughout product lifecycle since holographic patterns resist fading, scratching, and environmental degradation under normal conditions. Companies can further enhance security by incorporating custom holographic designs featuring proprietary patterns, brand elements, or serialization that create unique identifiers impossible to replicate without authorization.
Exceptional Visual Appeal and Brand Differentiation

Exceptional Visual Appeal and Brand Differentiation

Holographic paper transforms ordinary packaging and printed materials into captivating visual experiences that immediately attract consumer attention and create memorable brand impressions. The dynamic rainbow effects and shifting color patterns generated by light interaction with holographic structures produce premium aesthetic qualities that communicate product value and brand sophistication. This striking visual presentation operates continuously without power requirements or special lighting, delivering consistent impact across diverse retail environments from brightly lit supermarkets to atmospheric boutique settings. Marketing research consistently demonstrates that holographic packaging elements significantly increase shelf visibility and consumer engagement, directly influencing purchase decisions in competitive product categories. The technology enables creative designers to implement various holographic patterns including seamless backgrounds, spot highlights, text emphasis, or integrated imagery that aligns with brand identity and campaign themes. Holographic paper supports multi-sensory brand experiences as consumers naturally interact with products to observe changing visual effects from different viewing angles, increasing handling time and emotional connection. Businesses benefit from enhanced perceived value as consumers associate holographic elements with premium quality and innovation, potentially justifying higher price points and improving profit margins. The material's versatility accommodates both subtle sophisticated applications and bold attention-demanding designs, providing flexibility across different product positioning strategies. Seasonal and limited edition products gain additional appeal through special holographic treatments that create collectible qualities and urgency in consumer purchasing behavior.
Sustainable and Production-Friendly Solution

Sustainable and Production-Friendly Solution

Modern holographic paper delivers environmental responsibility alongside visual and security benefits through recyclable substrate options and eco-conscious manufacturing processes. Leading manufacturers now produce holographic paper using biodegradable metallized layers and water-based adhesives that maintain full recyclability within standard paper waste streams, addressing corporate sustainability commitments and consumer environmental concerns. This ecological compatibility eliminates the traditional trade-off between premium presentation and environmental stewardship, allowing brands to pursue both objectives simultaneously. Production efficiency represents another significant advantage as holographic paper integrates seamlessly with conventional printing and converting equipment without requiring specialized machinery investments or extensive operator retraining. The material demonstrates excellent printability across multiple technologies including offset, flexographic, gravure, and digital printing systems, accepting standard inks and coatings while maintaining holographic effect integrity. Converting operations proceed smoothly with holographic paper performing reliably through die-cutting, folding, gluing, and finishing processes used in packaging production. This operational compatibility reduces implementation barriers and accelerates time-to-market for new product launches or packaging redesigns. Holographic paper also offers favorable cost-performance ratios compared to alternative premium substrates or multiple-process security solutions, providing budget-conscious brands access to sophisticated presentation and protection capabilities. The material's proven shelf stability ensures holographic effects and printed graphics maintain appearance quality throughout extended storage periods and distribution cycles, minimizing waste from product degradation and supporting inventory management efficiency.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Interested Products
Please enter your interested products
Message
0/1000